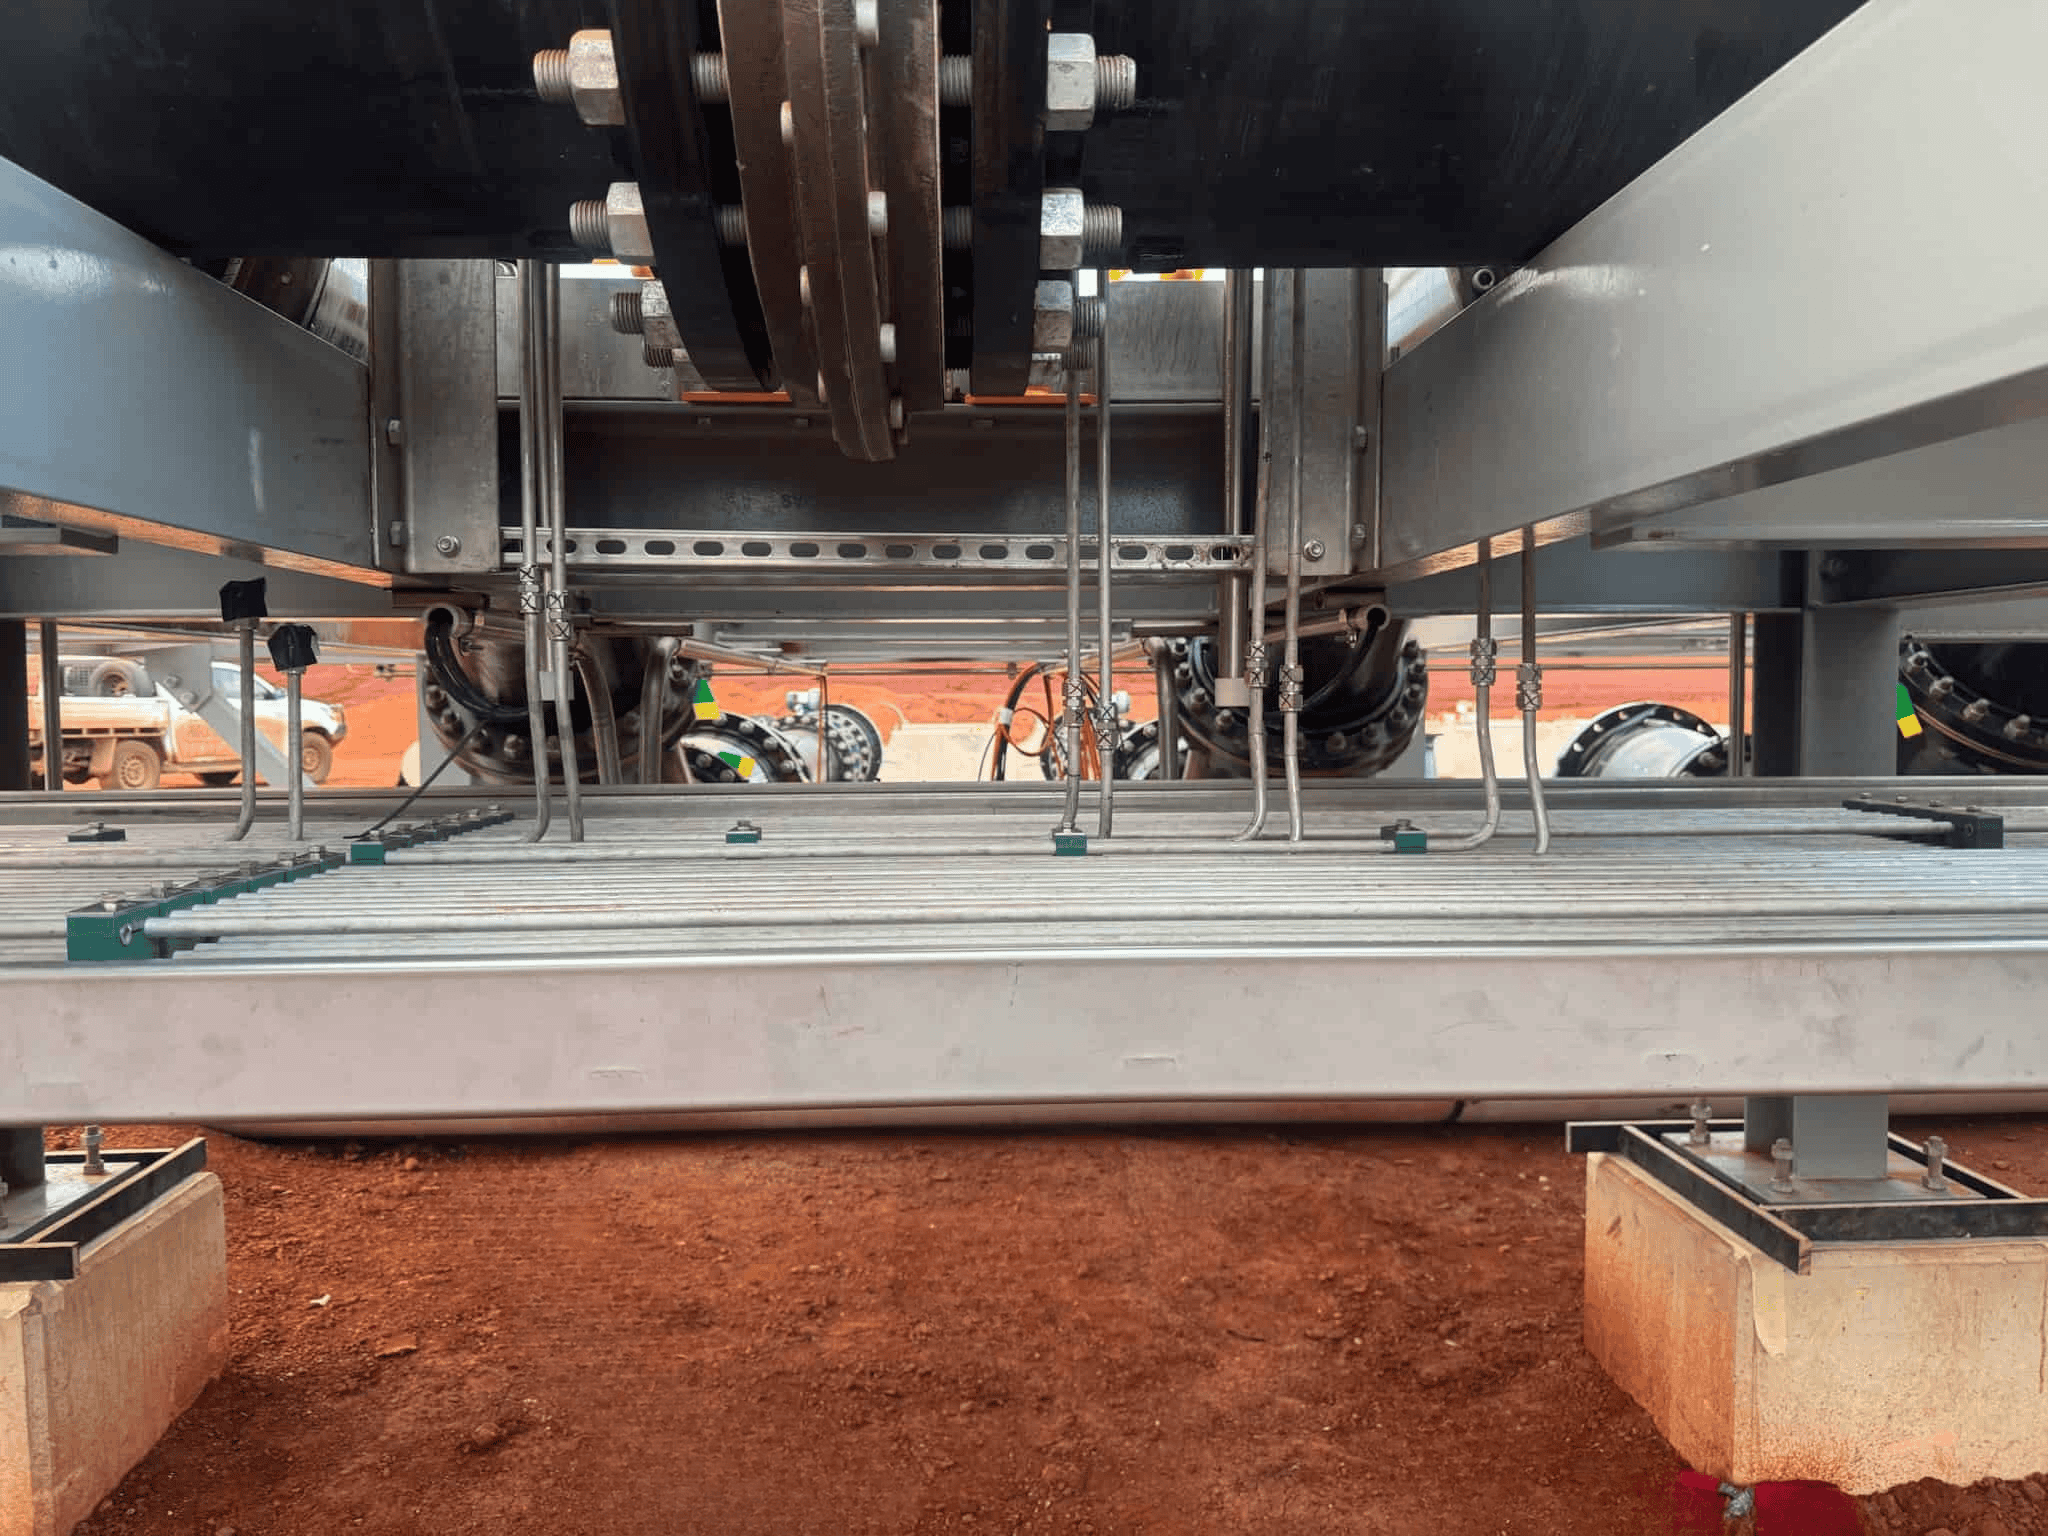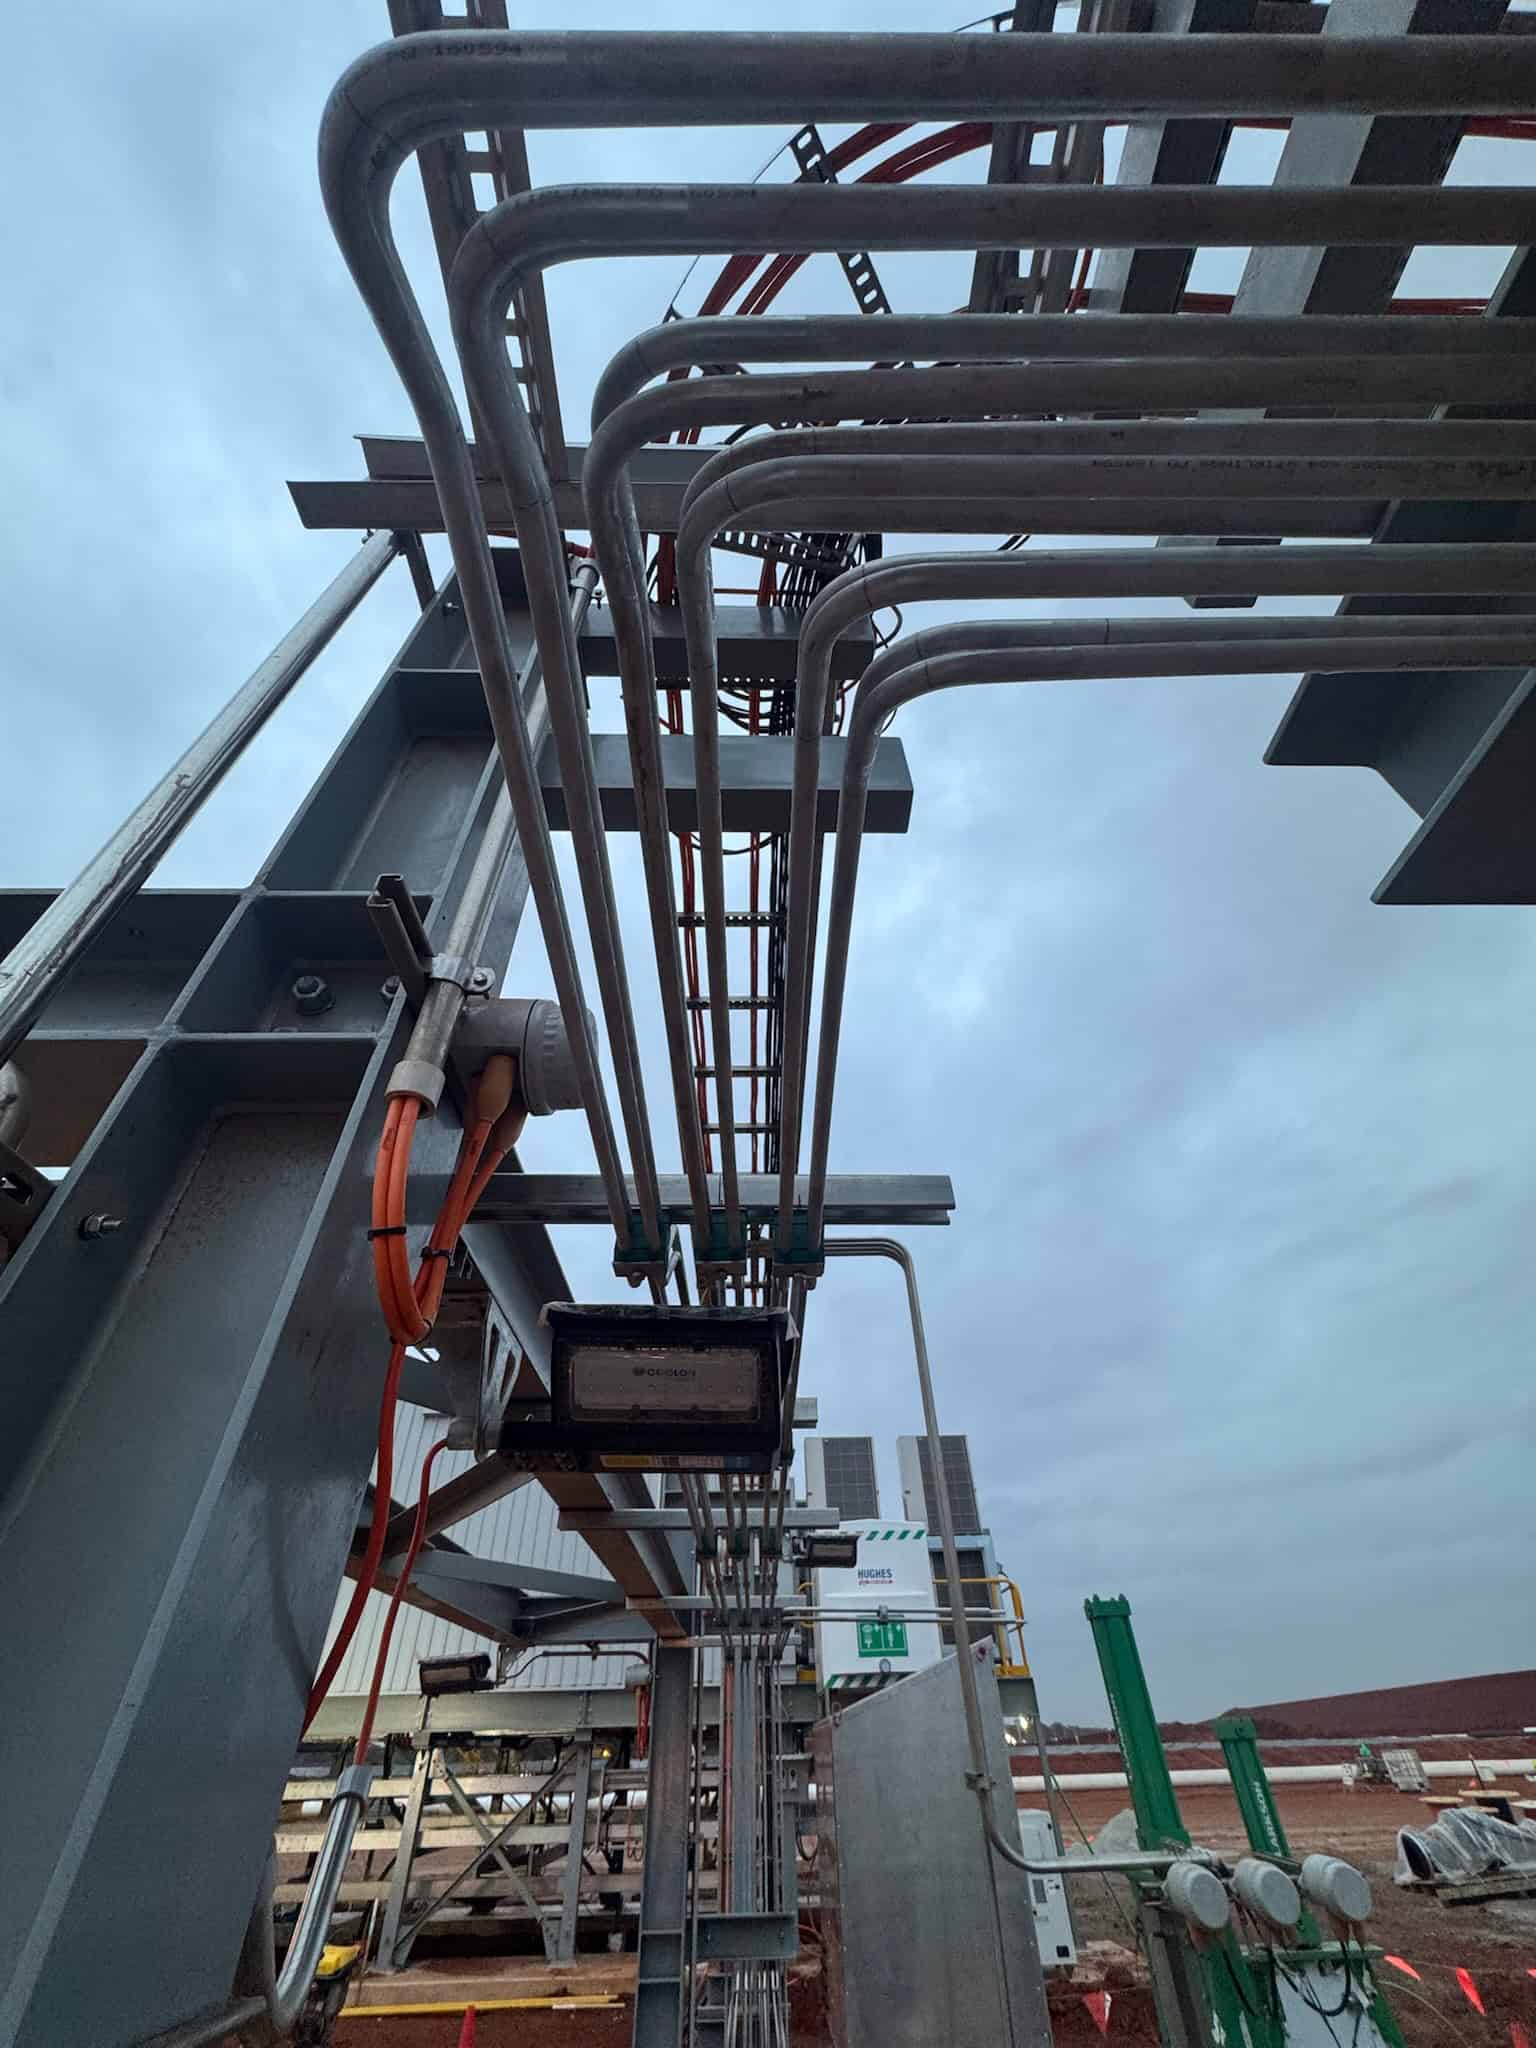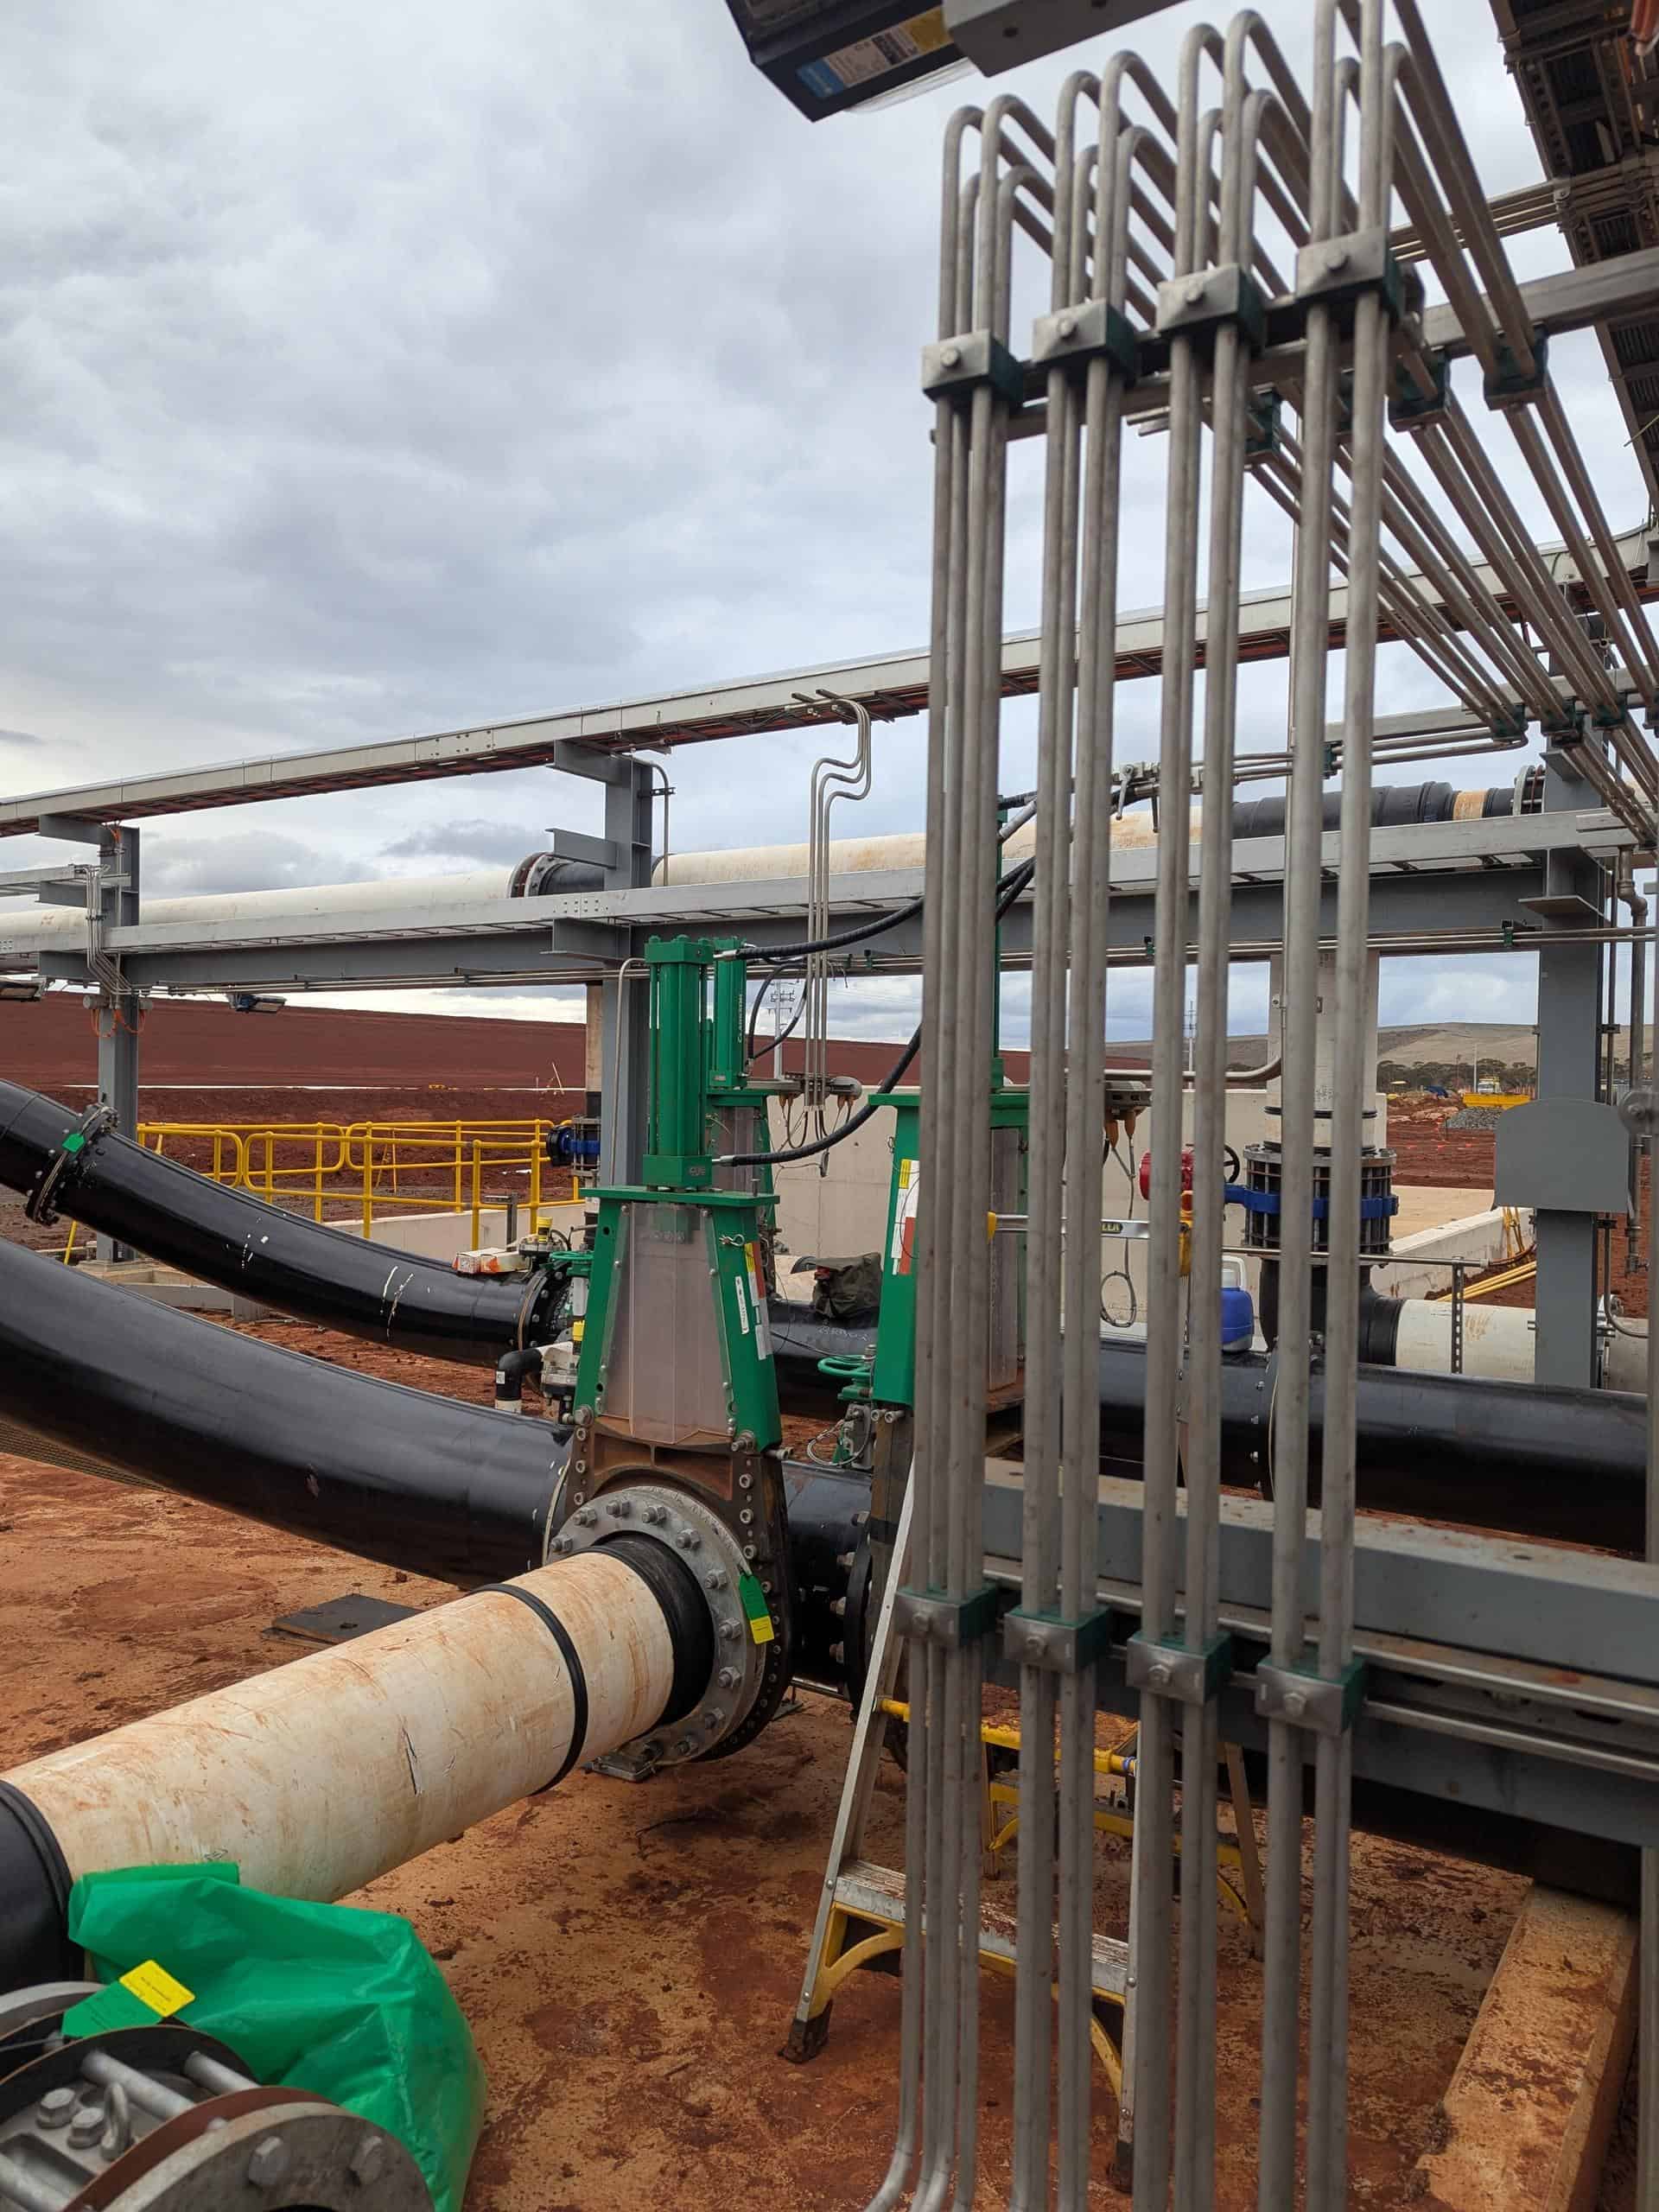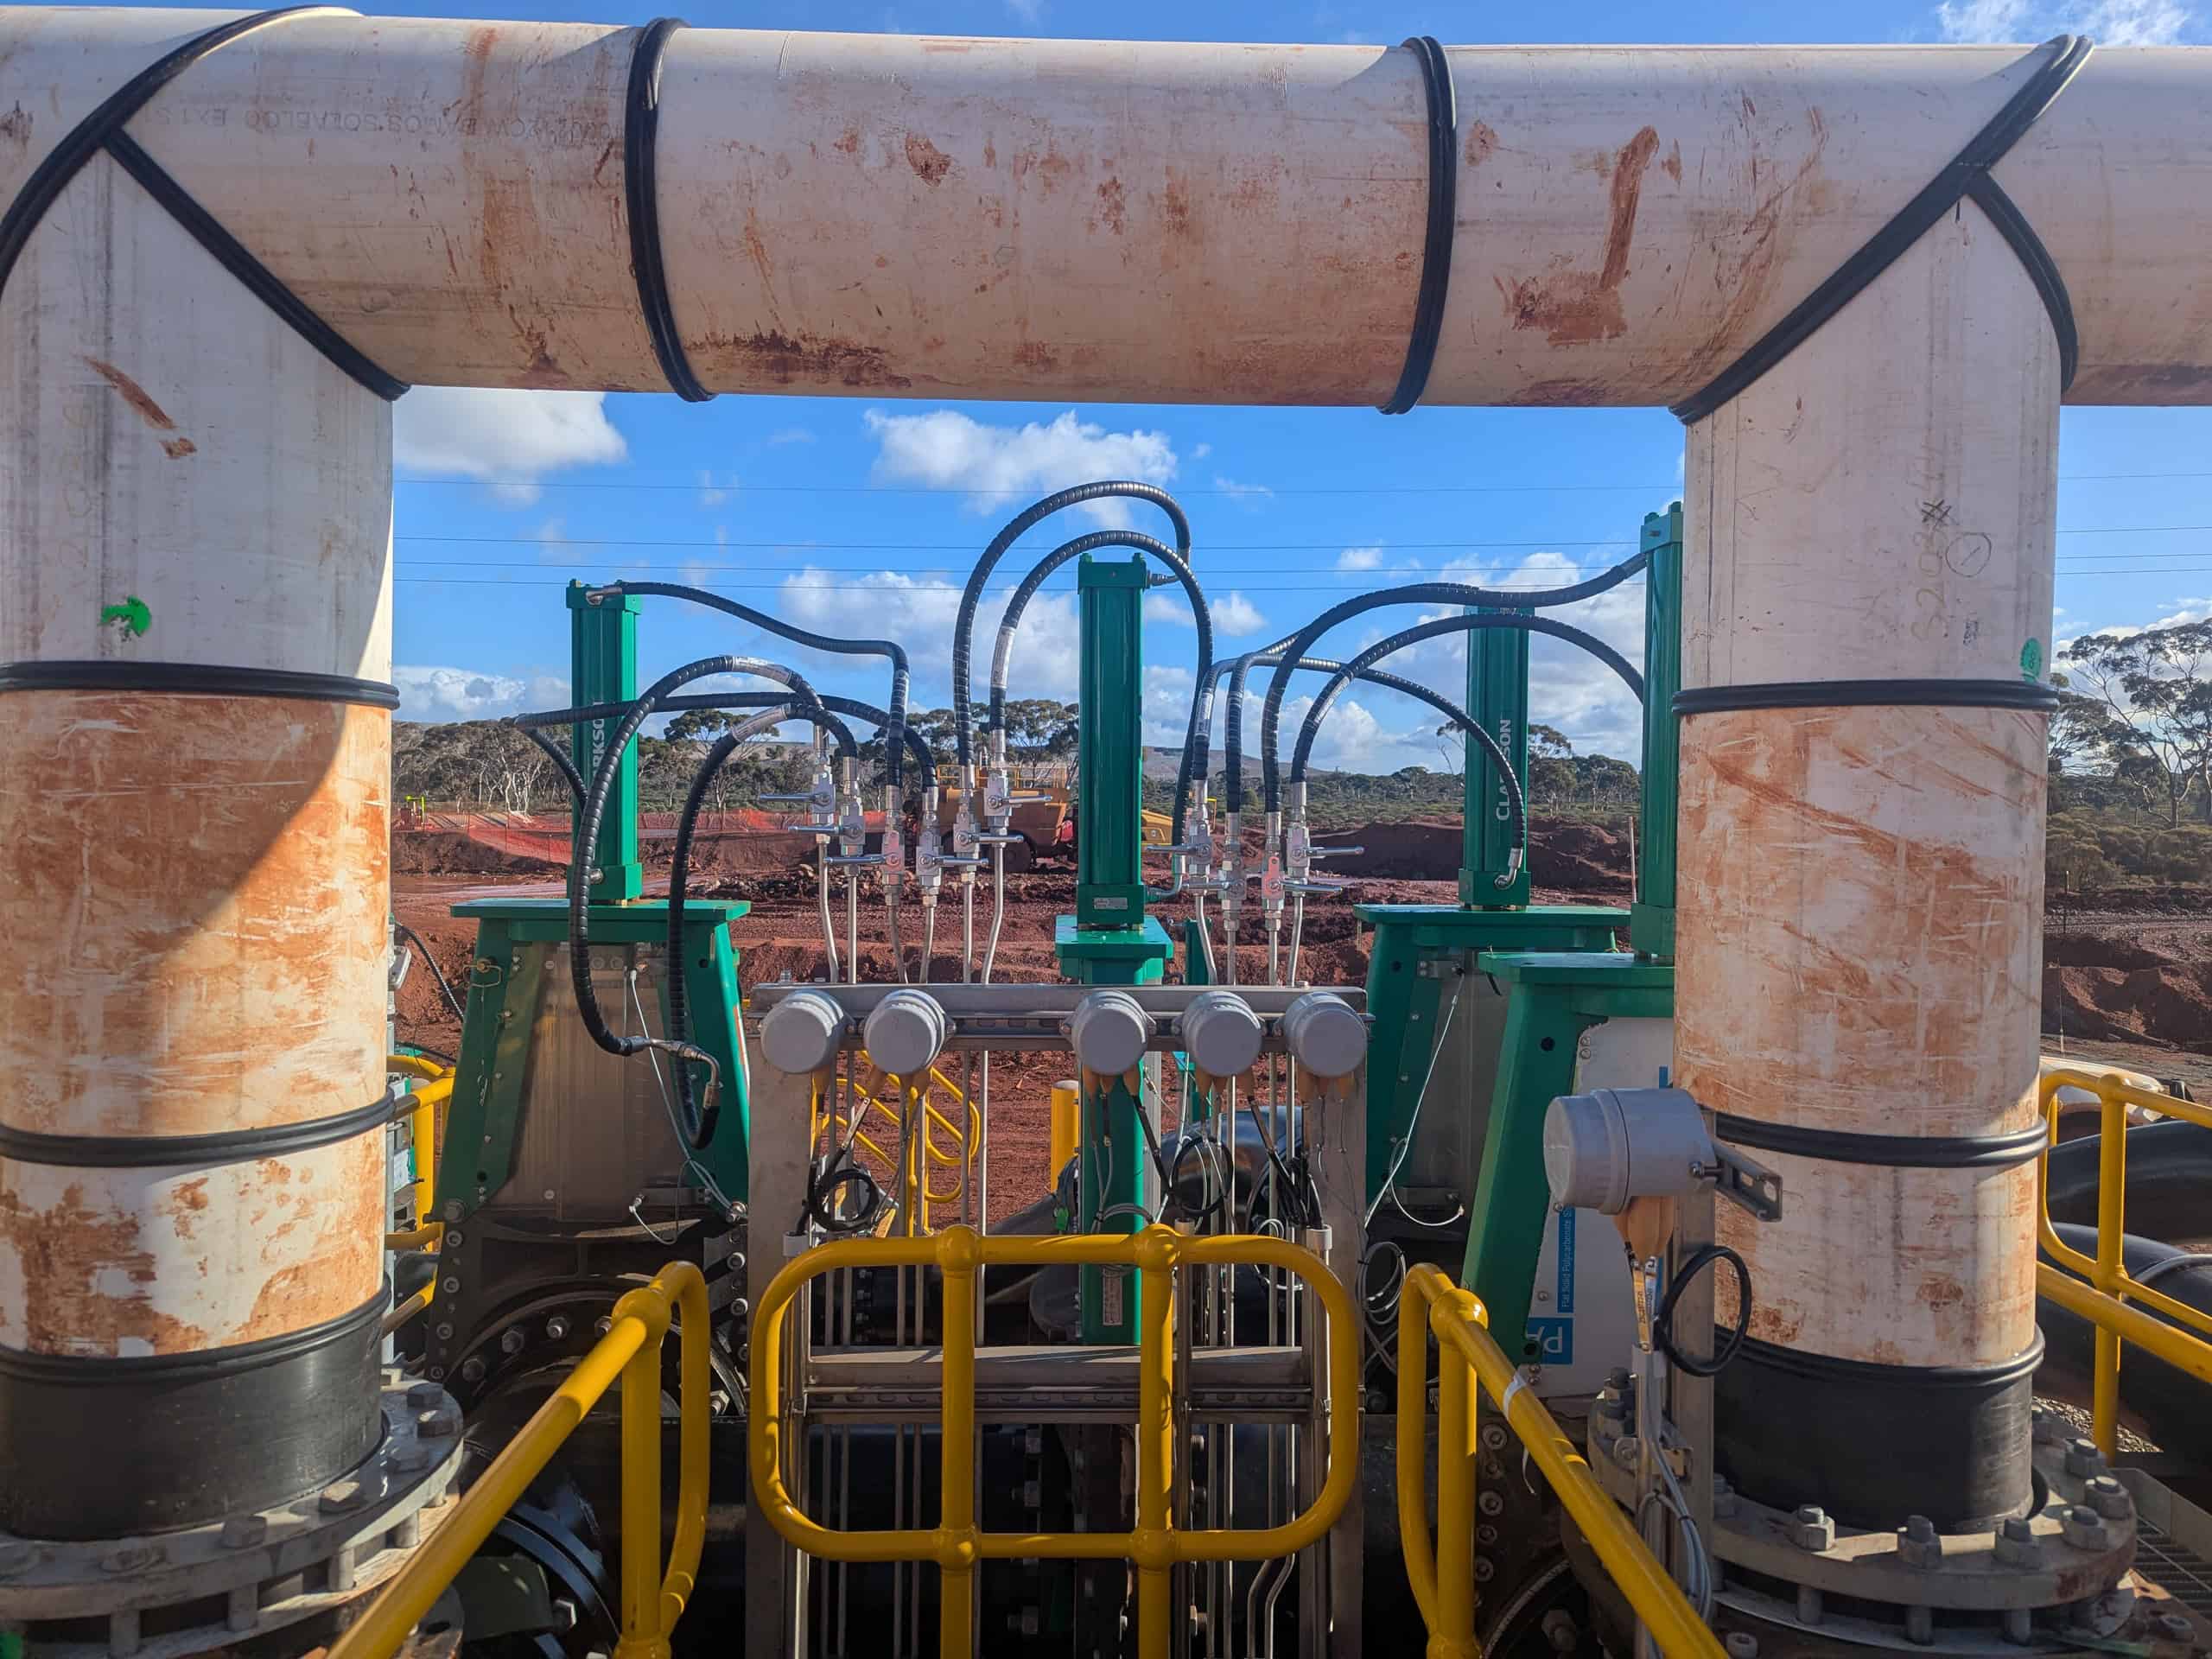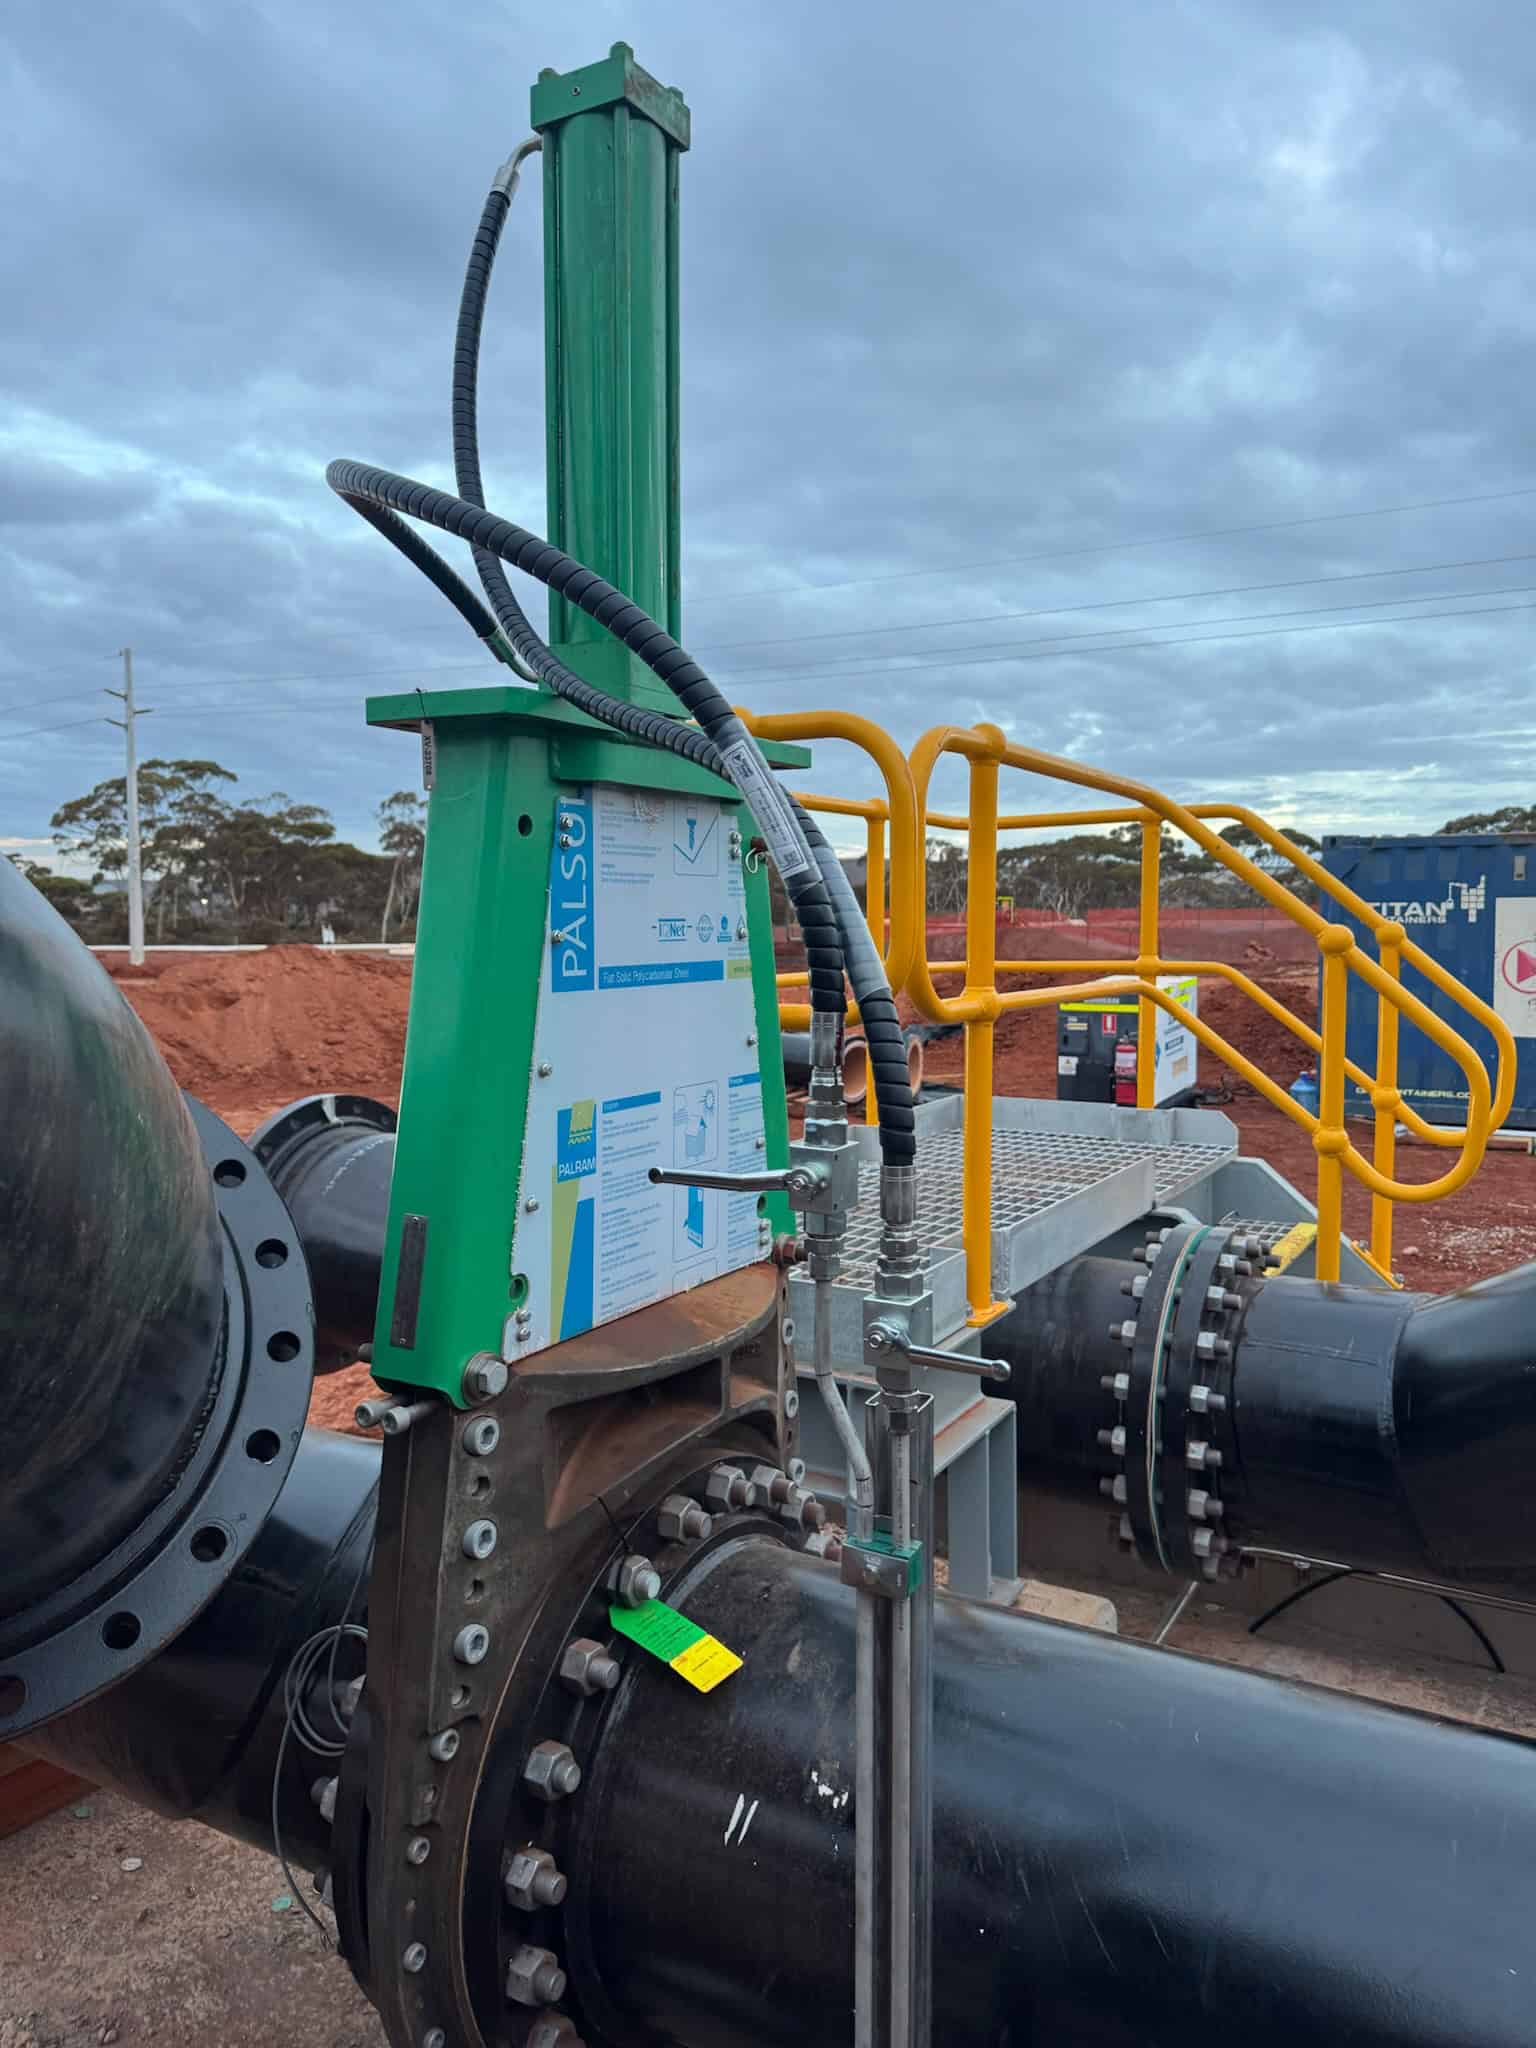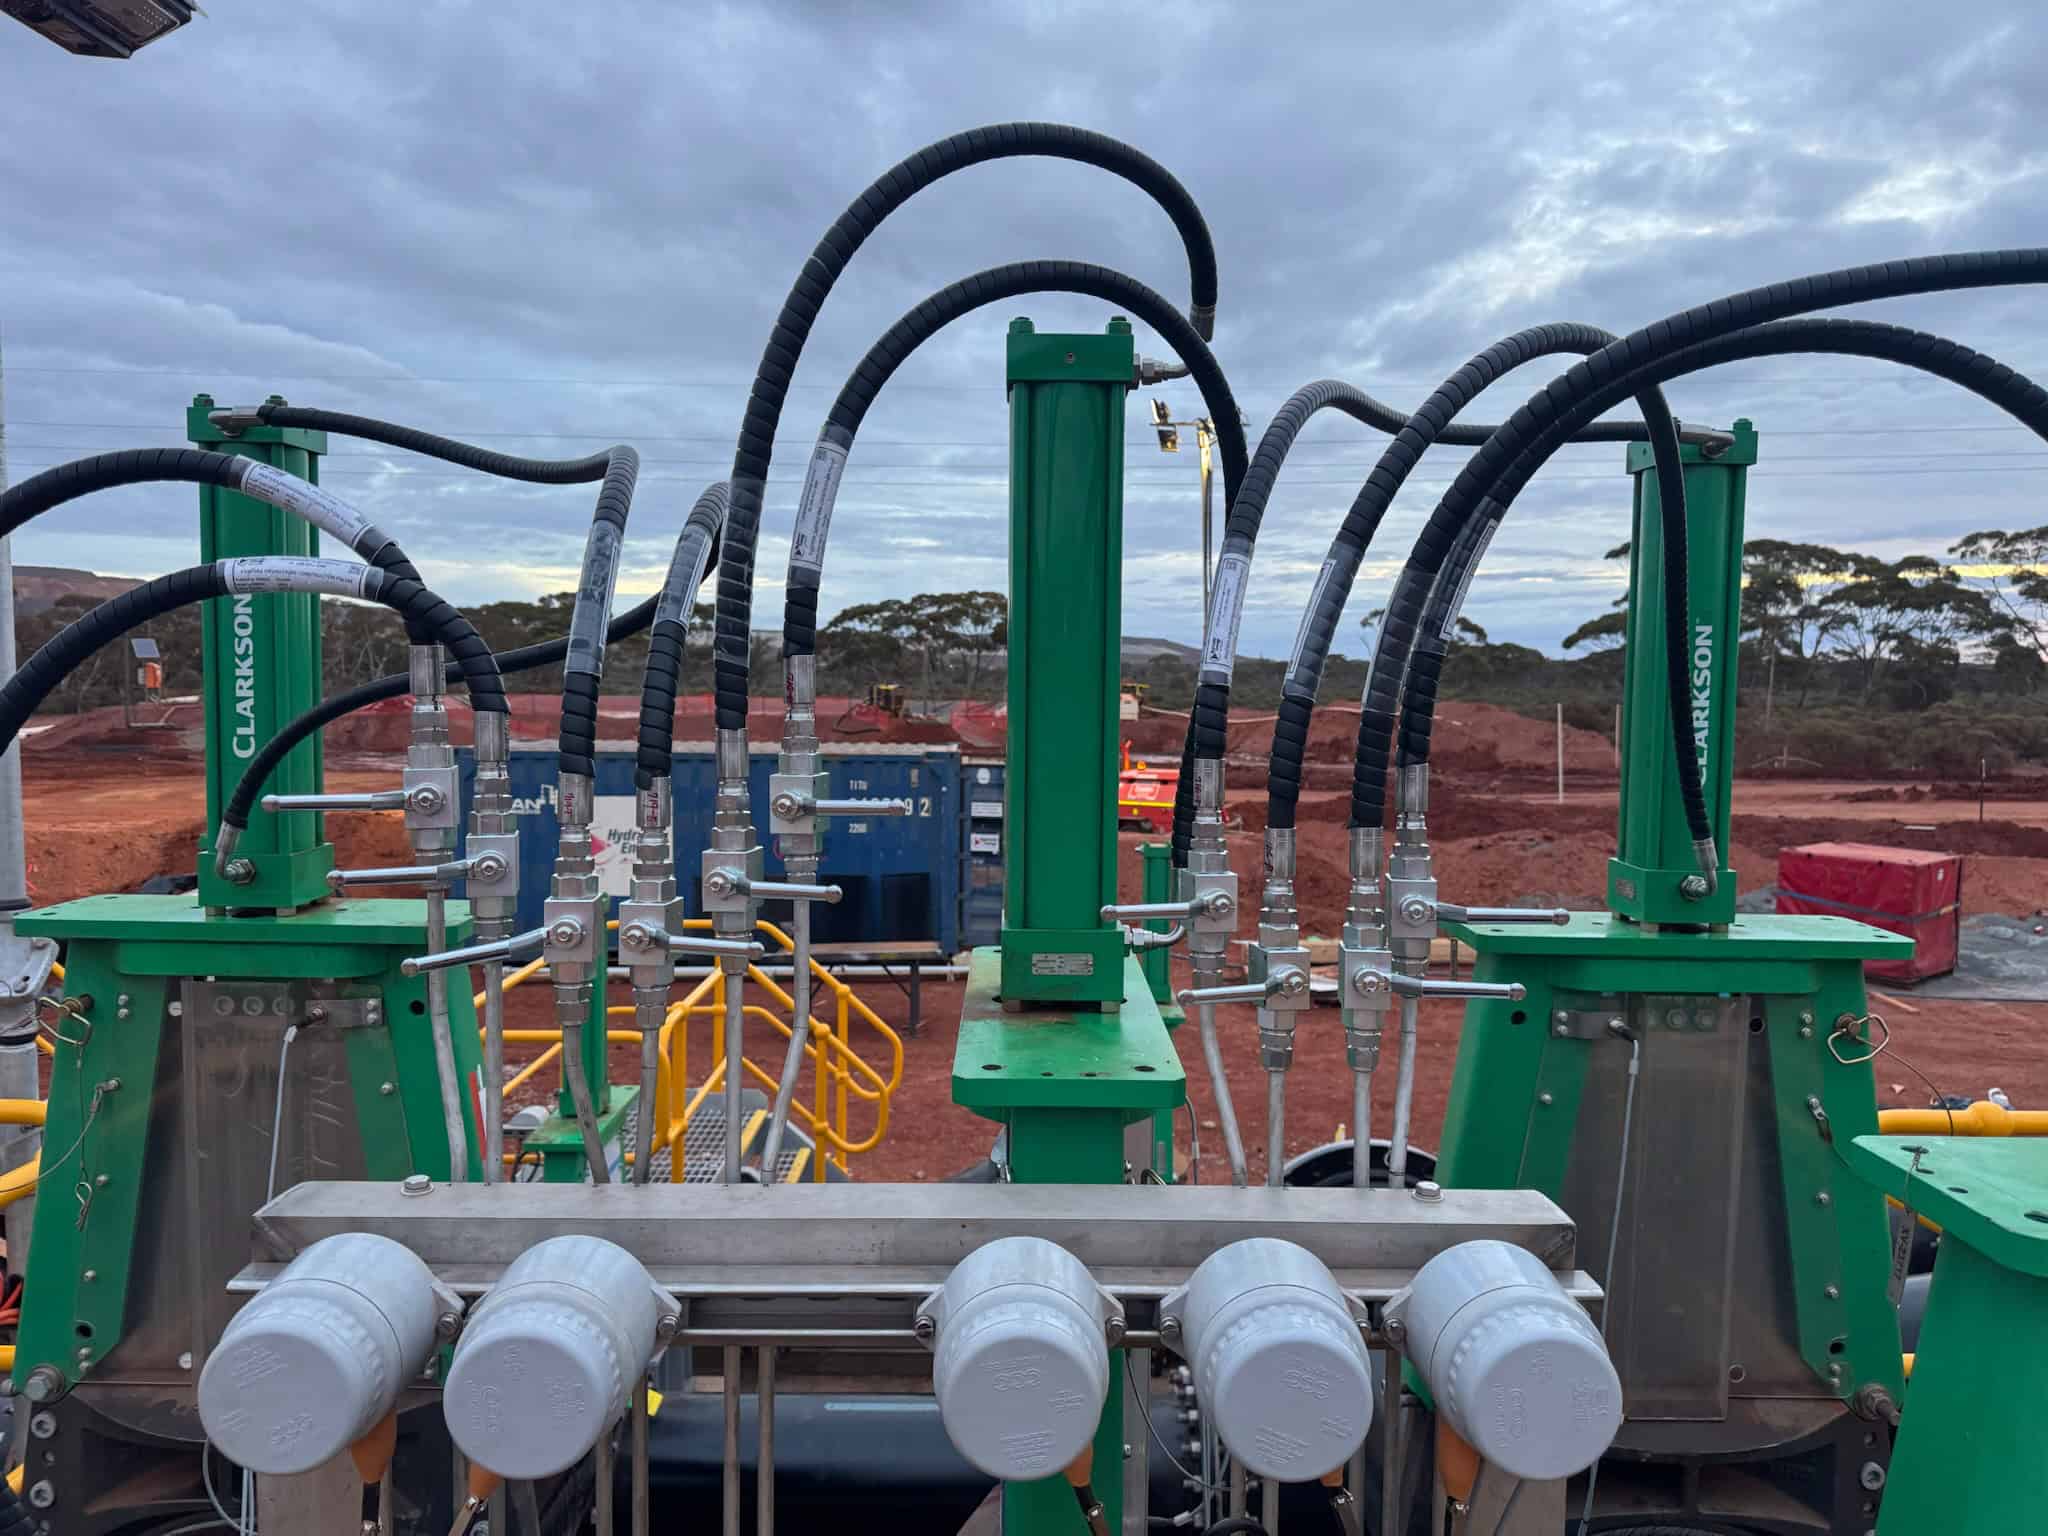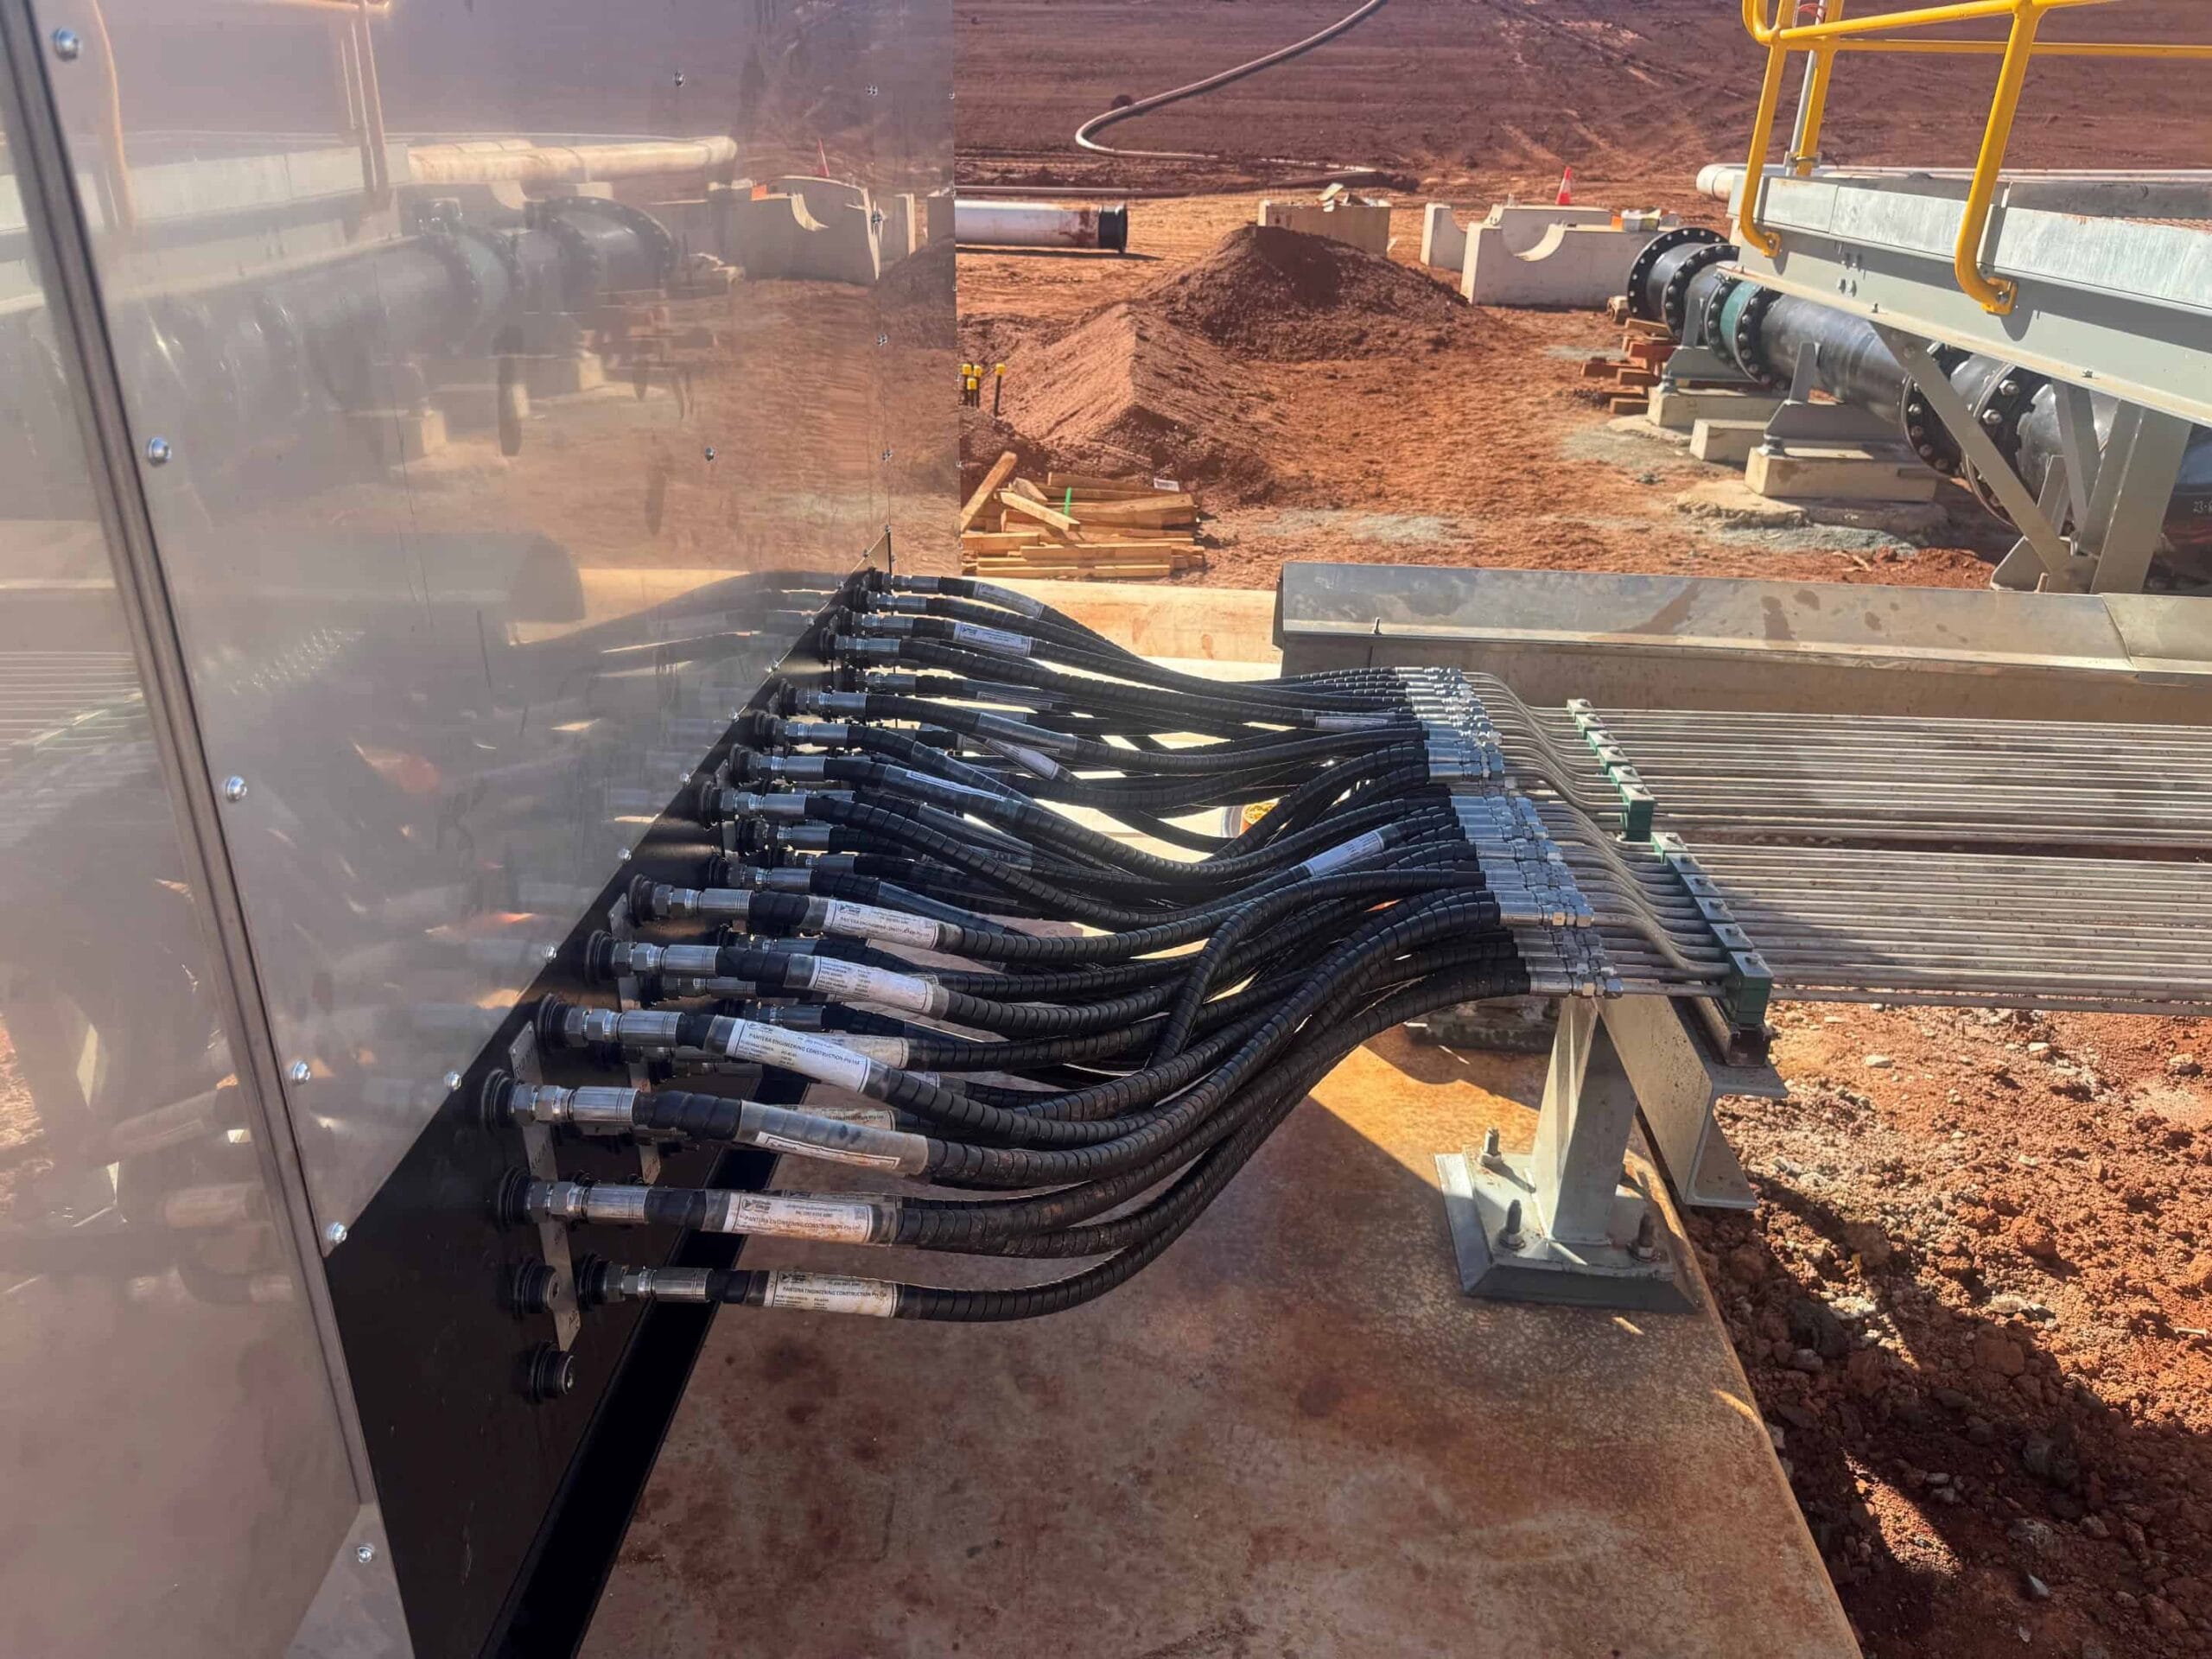
Hydraulic Energy Australia completed a fast-track hydraulic tubing installation across two locations at a mining site, covering a Valve Station and a Booster Pump Station. The scope encompassed engineering, procurement, fabrication, and full site execution, with over 1,000 metres of SS316 hydraulic tubing hand-bent and installed on site to serve 31 knife gate valve actuators.
PROJECT OVERVIEW
The project required a comprehensive, site-executed approach to hydraulic infrastructure across two stations. HEA managed the full scope from detail design and procurement through to installation, flushing, pressure testing, and documentation.
All SS316 tubing was hand-bent on site by HEA technicians to navigate the complex structural frameworks of each module. Custom structural support frames, SS316 Unistrut, and Stauff twin-clamp configurations were used throughout to ensure a clean, supported installation across both stations.
Hydrostatic pressure testing was carried out to 1.5 times design pressure, followed by controlled flushing to achieve an ISO 4406 cleanliness target of 17/15/12. A dedicated site team with mobile workshop facilities managed all on-site fabrication, hose crimping and tagging, and testing throughout the campaign.
Key Features
- Detail Design and Engineering: Installation methodology, procedures, and inspection and test plan developed prior to mobilisation.
- Procurement and Supply: Complete SS316 tubing, Hylok compression fittings, custom structural support frames, and Quintolubric 888-68 synthetic fluid supplied as part of the scope.
- Site-Fabricated Tubing: Over 1,000 metres of 1/2″ SS316 tubing hand-bent and installed on site to navigate complex structural module frameworks across both stations.
- Pressure Testing: Hydrostatic pressure testing completed to 1.5 times design pressure across all circuits.
- System Flushing and Cleanliness Verification: Controlled flushing carried out to achieve ISO 4406 cleanliness target of 17/15/12.
- Mobile Workshop Capability: On-site fabrication, hose crimp and tag, and testing managed from a dedicated mobile workshop facility throughout the campaign.
- Full Documentation: Complete MDR documentation package prepared and delivered on project completion.
This project is a good example of HEA’s ability to self-perform complex hydraulic infrastructure works in the field, combining Perth-based engineering and procurement with dedicated site execution. From initial design through to final testing and handover, our team delivered a clean, compliant installation on a tight schedule. Contact our team to discuss your next site hydraulic project.